

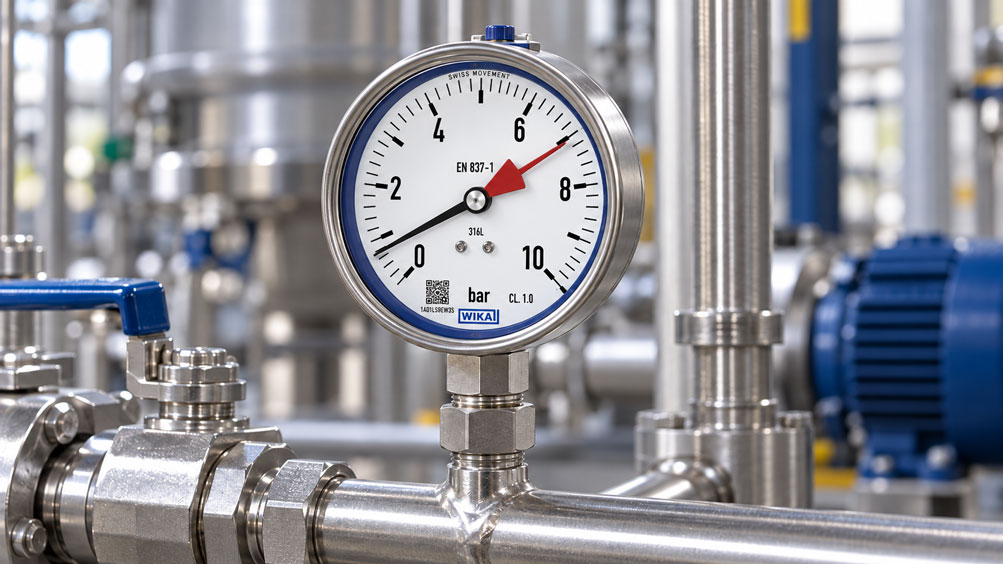
A hydraulic power unit normally operates at approximately 110 bar. The installed pressure gauge indicates a stable operating pressure. However, after several switching operations, the red maximum pointer remains at 160 bar, while the black measuring pointer has returned to 110 bar. Did the system actually reach a maximum pressure of 160 bar? Could the real pressure peak have been even higher? And can the position of the maximum pointer reveal how long the pressure increase lasted?
Questions like these frequently arise in mechanical engineering, hydraulic systems, pumps, compressors and pneumatic control systems. A pressure gauge with a maximum pointer is a practical solution in such applications, making temporary pressure increases visible even after they can no longer be detected by reading the normal pressure gauge pointer.
The operating principle initially appears straightforward: an additional pointer, usually red, is mechanically carried along by the normal measuring pointer as the indicated pressure increases. When the pressure subsequently decreases, the maximum pointer remains at the highest position reached. This allows an operator to recognize that a higher pressure indication occurred, even after the event has ended.
However, one crucial point is frequently overlooked: The maximum pointer records the highest indicated value reached by the mechanical measuring mechanism. It does not guarantee that the actual highest process pressure has been fully captured.
The Bourdon tube, pointer mechanism and maximum pointer have finite response speeds. During short pressure spikes, inertia, friction, movement damping, case filling and the dynamic behavior of the connecting line can cause the pressure peak to be displayed with reduced amplitude. Under certain dynamic conditions, mechanical oscillations can also contribute to excessive pointer deflection.
Another common mistake is to confuse the maximum pointer with a red reference pointer or an electrical switching contact. A maximum pointer mechanically retains a pointer position. It does not automatically monitor a safety limit and, without additional functions specifically designed for that purpose, does not generate an electrical signal.
For reliable selection, the measuring principle, expected duration of pressure spikes, permissible operating pressure, frequency of pressure cycling, media compatibility, installation conditions and required level of protection must therefore be considered together.
This technical article explains the function of a mechanical maximum pointer, its physical limitations and the differences between a retained indicated value and the actual maximum pressure reached. A detailed calculation example demonstrates how significantly a short pressure spike can be underestimated due to the dynamic behavior of a measuring system. It also covers correct sizing, typical fault symptoms, testing procedures and suitable pressure gauges from the ICS product range.
Table of Contents
- Measurement Tasks and Typical Problems with Maximum Pointer Pressure Gauges
- Physical Principles of Mechanical Pressure Measurement
- Understanding How a Maximum Pointer Works
- Distinguishing Maximum Pointers, Reference Pointers and Peak Value Memory
- Causes of Misinterpreted Maximum Values
- Installation, Process Connections and Ambient Conditions
- Selecting Measuring Range, Accuracy Class and Overpressure Resistance
- Practical Example: Calculating a Short Pressure Spike and the Indicated Maximum Value
- Distinguishing Pressure Spikes, Pulsations and Pressure Surges
- Pointer Inertia, Friction and Mechanical Hysteresis
- Evaluating Case Filling, Restrictors and Pressure Snubbers
- Influence of Measuring Lines and Connection Volumes
- Process Media, Materials and Temperature Limits
- Correctly Resetting and Documenting the Maximum Pointer
- Dynamic Measurement and Electronic Peak Value Detection
- Calibration, Functional Testing and Repeatability
- Measurement Uncertainty and the Significance of the Retained Maximum
- Operational Safety, Protective Functions and Limit Values
- Typical Applications in Mechanical and Plant Engineering
- Systematic Testing and Commissioning Procedure
- Typical Fault Symptoms and Targeted Diagnostics
- Suitable ICS Products and Selection Options
- Conclusion: Using the Maximum Pointer Correctly as a Diagnostic Indicator
- Frequently Asked Questions About Pressure Gauges with Maximum Pointers
1. Measurement Tasks and Typical Problems with Maximum Pointer Pressure Gauges
A conventional mechanical pressure gauge indicates the pressure currently acting at its measuring point. Once the pressure has returned to normal after a brief increase, the previous event can no longer be detected from the regular measuring pointer.
This is precisely where the maximum pointer becomes useful. It makes the highest mechanically reached indication visible since its last reset.
Typical measurement tasks include:
- Determining whether a hydraulic system has temporarily reached higher indicated pressures than during steady-state operation.
- Detecting unusual pressure increases following valve or pump switching operations.
- Comparing maximum indications between maintenance intervals.
- Checking whether pressure control systems cause unexpected pressure increases.
- Supporting troubleshooting of pressure switches, pressure relief valves and control operations.
- Monitoring machinery that is not continuously attended by an operator.
- Adding a simple mechanical maximum value indication to an existing pressure measuring point.
However, the actual requirement must be defined more precisely. Is the purpose simply to determine whether the pressure indication exceeded a certain value? Should the highest slowly changing pressure indication be documented? Or must a pressure spike lasting only a few milliseconds be captured reliably and with a known uncertainty?
These measurement tasks may require different instruments.
For the first task, a maximum pointer pressure gauge may be entirely sufficient. However, accurately detecting very short pressure transients may require a pressure sensor with suitable dynamic characteristics and sufficiently fast data acquisition.
It is particularly problematic to claim that the red pointer proves that the process pressure never exceeded a specific higher value. Without knowing the dynamic characteristics of the pressure gauge, such proof is not possible.
A maximum pointer can therefore be a valuable diagnostic instrument but must not automatically be treated as a precision pressure peak recorder.
2. Physical Principles of Mechanical Pressure Measurement
Many industrial pressure gauges are Bourdon tube pressure gauges. They operate using an elastic measuring element whose deformation depends on the applied pressure.
2.1 Bourdon Tube as a Pressure-Sensing Element
The Bourdon tube typically has a flattened tube cross-section and a curved shape.
As the internal pressure increases, its curvature changes. The free end of the Bourdon tube moves and transfers this movement to the pointer mechanism.
A mechanical transmission converts the relatively small movement of the measuring element into an easily readable rotational movement of the pointer.
Bourdon tube pressure gauges are available for many different pressure ranges. The actual permissible operating and overpressure conditions depend on the specific configuration.
2.2 Pressure and Elastic Deformation
Within the intended measuring range, the deformation of the measuring element is used to indicate pressure.
Calibration determines how much the indication deviates from the reference value at defined static reference pressures.
However, rapid pressure changes introduce an additional factor: the measuring element and mechanical pointer transmission require time to follow the pressure change.
2.3 Dynamic Behavior
A real pressure gauge is not a massless measuring system with instantaneous response.
The components involved have mass, stiffness, friction and damping. Their movement during a rapid pressure change can therefore differ from the actual pressure profile.
The magnitude of this deviation depends on the device configuration and the time-dependent characteristics of the pressure event.
2.4 Consider the Pressure Reference
A conventional Bourdon tube pressure gauge is frequently designed to measure gauge pressure.
Absolute pressure, gauge pressure and differential pressure are different measured quantities.
When comparing the gauge with an electronic reference sensor, the pressure type, unit and measuring range must therefore match or be correctly converted.
3. Understanding How a Maximum Pointer Works
A mechanical maximum pointer, also known as a drag pointer, is an additional pointer that retains the highest indicated value reached during the observation period.
For corresponding configurations, WIKA describes a maximum pointer that is moved by the normal measuring pointer via a driving pin.
3.1 Behavior During Increasing Pressure
As the process pressure increases, the normal measuring pointer moves toward higher scale values.
When the measuring pointer reaches the position of the maximum pointer, it carries the maximum pointer along through the mechanical driving mechanism.
If the indication continues to increase, both pointers move together toward the higher pressure value.
3.2 Behavior During Decreasing Pressure
When the pressure decreases, the measuring pointer moves back.
The maximum pointer, however, remains in its previously reached position due to its mechanical retaining mechanism.
The instrument therefore simultaneously provides two pieces of information:
- The pressure currently indicated by the main pointer.
- The highest indicated value reached and retained by the measuring mechanism since the last reset.
3.3 Meaning of the Retained Value
The maximum pointer does not store a sequence of measured values, the time of an event or its duration.
The number of pressure spikes cannot be determined from it either.
For example, if the maximum pointer remains at 140 bar, this may mean that the measuring mechanism reached this value once or that numerous pressure events occurred up to this indicated value.
Without an additional measurement, it is not possible to distinguish between these situations.
3.4 Limitations of Mechanical Maximum Value Memory
A short pressure surge may be over before the complete mechanical measuring system reaches the corresponding pointer position.
In addition, the extra frictional torque and dynamic movement of the measuring mechanism can influence the retained position.
The maximum pointer is therefore a mechanical maximum value memory for the indication, not automatically a validated peak pressure measuring instrument for arbitrarily fast process pressure profiles.
4. Distinguishing Maximum Pointers, Reference Pointers and Peak Value Memory
Pressure gauges are available with various additional pointers and indication functions. Their purposes differ significantly.
In particular, a red reference pointer must not be confused with a red maximum pointer.
| Configuration | Operating Principle | What Is Indicated? | Important Limitation |
|---|---|---|---|
| Normal measuring pointer | Mechanical movement corresponding to the pressure-sensing element | Current pressure indication | Previous pressure spikes are no longer visible after the pointer returns |
| Mechanical maximum pointer | Mechanical driving and retention of the highest pointer position reached | Highest mechanically indicated pressure since the last reset | Very short pressure spikes may not be fully captured, depending on measurement dynamics |
| Reference pointer | Fixed or manually adjustable marker | Preset reference or limit value | Normally does not store an actual maximum value reached |
| Contact pressure gauge | Mechanically or electronically actuated switching contact | Switching status at a specified pressure threshold | Switching function and response behavior must be specified separately |
| Digital maximum value memory | Electronic storage of processed measurement values | Highest value captured by the device since the last reset | Sampling rate, measurement bandwidth and filtering determine peak detection |
| Dynamic pressure sensor with data acquisition | Time-resolved acquisition of the pressure signal | Pressure profile including suitable transient events | Sensor, installation, sampling rate and signal processing must be sufficiently fast |
4.1 Reference Pointer
A reference pointer is used to highlight a particular pressure value on the scale.
For example, it can serve as a visual indication of a setpoint or an intended operating limit.
However, it does not necessarily follow the measuring pointer and does not store a maximum value.
4.2 Mechanical Maximum Pointer
The maximum pointer records the highest indication reached by the main pointer and mechanically transferred to it.
It therefore provides a retrospectively readable indication of the pressure behavior since its last reset.
4.3 Electronic Peak Value Function
An electronic measuring instrument can store minimum and maximum measured values.
Here too, it must be checked at what measurement rate values are captured and whether upstream filters reduce short pressure spikes.
A digitally displayed maximum value is not automatically the actual highest process pressure.
4.4 Switching and Protective Functions
A maximum pointer does not automatically provide an alarm function.
If exceeding a pressure limit must shut down a machine or protect a process, suitable switching or safety equipment must be provided for that purpose.
5. Causes of Misinterpreted Maximum Values
The position of the maximum pointer can deviate from the actual highest process pressure for various reasons.
5.1 Pressure Spike Too Short
If a pressure event lasts considerably less time than the mechanical measuring system’s response time, the main pointer may not reach the actual pressure peak.
The maximum pointer may then remain below the true maximum pressure.
5.2 Friction and Retaining Torque
The maximum pointer must be moved against a mechanical retaining force.
This can influence its movement. A stiff maximum pointer may fail to register smaller or short excursions reliably.
5.3 Oscillation and Overshoot
The pointer mechanism can oscillate under dynamic loading.
Depending on the system behavior, the pointer deflection can temporarily exceed the quasi-static indication corresponding to the same pressure.
Such an excessive indication must not automatically be interpreted as a real pressure spike.
5.4 Damping
Case fillings, restrictors and pressure snubbers influence the time-dependent movement of the measuring system.
They may be necessary for service life and readability but can make the full indication of short pressure events more difficult.
5.5 Unknown Observation Period
If the last reset time of the maximum pointer has not been documented, it is unknown which operating period the maximum value relates to.
The indicated highest value may then originate from an event that occurred a long time ago.
5.6 Unnoticed Reset
If the maximum pointer is reset between two readings without documentation, information about the previous maximum value is lost.
5.7 Previous Damage to the Pressure Gauge
A pressure gauge that has already been subjected to impermissible overpressure or mechanical damage may exhibit altered indication characteristics.
A seemingly correct current pointer position therefore does not prove that the instrument is still operating within its specification.
6. Installation, Process Connections and Ambient Conditions
Correct installation directly influences measurement reliability and the service life of a maximum pointer pressure gauge.
6.1 Suitable Measuring Point
The pressure gauge must be installed at a location where the pressure is actually representative of the intended measurement.
In hydraulic systems, different time-dependent pressure profiles can occur upstream and downstream of valves, restrictors and pumps.
A maximum pointer at an unsuitable measuring point may therefore respond correctly to local pressure changes but fail to capture the process variable of interest.
6.2 Mounting Position
For mechanical pressure gauges, the mounting position and pointer mechanism design can influence the indication.
The mounting position specified by the manufacturer or the reference position used during calibration must be considered.
6.3 Mechanical Loading
Pipelines must not transmit impermissible mechanical forces or moments to the process connection.
For machines exposed to strong vibrations, suitable mounting at a less vibration-prone location may be necessary.
6.4 Readability
The red maximum pointer and the normal measuring pointer must be clearly distinguishable.
A clearly readable dial, sufficient lighting and a suitable nominal size make evaluation easier.
Larger nominal sizes may be useful when readings frequently have to be taken from a greater distance.
6.5 Process Connection
Thread dimensions, sealing principle and material must match the existing process connection.
A G-thread with a suitable sealing surface is not automatically interchangeable with an NPT thread.
The pressure gauge must be mounted at the intended connection according to the manufacturer’s instructions. Impermissible installation forces on the case or window must be avoided.
6.6 Isolation and Maintenance Options
Suitable pressure gauge valves or shut-off valves may be provided for maintenance and testing.
Their suitability and permissible operation depend on the medium, pressure, temperature and design of the complete measuring point.
Before removal, the system must be confirmed depressurized according to the specified procedure.
7. Selecting Measuring Range, Accuracy Class and Overpressure Resistance
The measuring range must adequately cover both normal process pressure and expected pressure increases.
A scale selected too narrowly may result in pressure indications outside the intended display range during peak events.
Conversely, choosing an unnecessarily large measuring range can reduce readability and absolute resolution.
7.1 Typical Operating Pressure
The first step in selection is to determine the pressure occurring during steady-state operation.
This value must not be confused with the maximum possible process pressure.
The manufacturer’s specifications and the intended pressure loading class of the gauge determine the permissible continuous load.
7.2 Continuous Pressure Loading
EN 837-1 distinguishes between Bourdon tube pressure gauges that can be continuously loaded up to full scale and versions with a lower permissible continuous load.
For gauges not rated for continuous full-scale loading, a limit of 75 % of full scale is typically relevant for continuous loading under the corresponding standard configuration.
This must not be applied to every pressure gauge without verification.
7.3 Overpressure Capability
Overpressure capability describes the pressure a gauge can withstand above its regular measuring range under certain specified conditions.
It is not equivalent to maximum accuracy or continuous pressure loading capability.
It is particularly important to distinguish between:
- Full-scale value or indication range.
- Maximum permissible operating pressure.
- Overpressure limit under specified test conditions.
- Safety-related pressure resistance and failure behavior.
A maximum pointer does not change these limits.
7.4 Accuracy Class
For a pressure gauge with accuracy class 1.0 according to EN 837-1, the permissible indication error under the applicable reference and test conditions typically corresponds to 1 % of full scale.
For an indication range of 0 to 250 bar, this gives:
Error limit = ±0.01 · 250 bar = ±2.5 bar
However, this static accuracy class must not be interpreted as a guaranteed accuracy of the maximum pointer indication for a short pressure surge.
7.5 Do Not Treat Full Scale as a Protective Function
A high full-scale value is no substitute for suitable pressure limitation.
Even an overpressure-resistant pressure gauge does not automatically make excessive process pressure loading permissible for the remaining system components.
8. Practical Example: Calculating a Short Pressure Spike and the Indicated Maximum Value
A hydraulic test bench is to be examined for short-term pressure increases following valve switching operations.
A mechanical Bourdon tube pressure gauge with a maximum pointer is used for local monitoring. In addition, a sufficiently fast electronic pressure sensor with suitable data acquisition is used for a reference investigation.
The question is why the maximum pointer can indicate a lower value even though a higher actual maximum pressure has occurred.
8.1 Initial Situation
The following freely selected values are explicitly assumed for this calculation example:
- Normal process pressure: 110 bar.
- Pressure gauge indication range: 0 to 250 bar.
- Assumed static accuracy class of the pressure gauge: 1.0.
- Actual pressure during an idealized rectangular pulse: 190 bar.
- Duration of the pressure pulse: 0.040 s or 40 ms.
- Pressure change relative to the initial condition: 80 bar.
- Simplified dynamic model: linear first-order system.
- Assumed time constant of the complete measuring system: 0.120 s.
- Assumed sampling rate for the comparison measurement: 1,000 samples per second.
These values do not describe any particular WIKA or ICS pressure gauge. In particular, the assumed time constant is not a guaranteed product characteristic.
The model serves exclusively to illustrate the principle of dynamic indication error in a comprehensible manner.
8.2 Calculate the Pressure Change
The initial pressure is:
p0 = 110 bar
During the assumed pressure pulse, the actual pressure reaches:
pmax = 190 bar
The pressure change is:
Δp = 190 bar – 110 bar
Δp = 80 bar
8.3 Simplified Dynamic Measurement Model
For an idealized first-order measuring system, the response to a sudden pressure increase can be described approximately by:
pindicated(t) = p0 + Δp · (1 – e-t/τ)
Where:
- p0 is the original pressure.
- Δp is the magnitude of the pressure step.
- t is the time elapsed since the beginning of the pressure step.
- τ is the assumed time constant.
The formula describes a simple delayed measurement response. A real mechanical pressure gauge can additionally exhibit friction, overshoot and other nonlinear effects.
8.4 Calculate the Indicated Pressure After 40 ms
For a pulse lasting 40 ms and the assumed time constant of 120 ms:
t / τ = 0.040 s / 0.120 s
t / τ = 0.3333
Therefore:
pindicated = 110 bar + 80 bar · (1 – e-0.3333)
With:
e-0.3333 ≈ 0.7165
This gives:
pindicated ≈ 110 bar + 80 bar · 0.2835
pindicated ≈ 132.68 bar
Although the actual pressure in the model briefly reaches 190 bar, the delayed mechanical indication only rises to approximately 133 bar during the 40-ms pulse.
A maximum pointer ideally driven by this indication would therefore retain approximately this lower value.
The actual maximum pointer of a real pressure gauge may behave differently because the simplified dynamic model used here does not describe all mechanical effects.
8.5 Difference Between Actual and Indicated Maximum
The difference between the assumed actual maximum pressure and the calculated indication is:
Δpdynamic = 190 bar – 132.68 bar
Δpdynamic ≈ 57.32 bar
Relative to the magnitude of the pressure pulse, only approximately 28.35 % of the change is indicated during the considered pulse duration.
This example demonstrates why the static accuracy class of a pressure gauge alone cannot provide a reliable statement about the complete detection of very short pressure spikes.
8.6 Calculate the Static Error Limit
For a pressure gauge with an indication range of 0 to 250 bar and accuracy class 1.0, the static error limit is:
±2.5 bar
The calculated dynamic deviation of approximately 57 bar is considerably larger.
This does not mean that the pressure gauge violates its static accuracy specification. A static test specification does not automatically describe the instrument’s behavior during a pressure pulse lasting only 40 ms.
8.7 Importance of Electronic Data Acquisition
A sampling rate of 1,000 samples per second corresponds to a time interval of:
Δt = 1 / 1,000 s
Δt = 0.001 s = 1 ms
An idealized 40-ms pressure pulse therefore contains approximately 40 sampling intervals.
Whether the actual pressure profile is correctly recorded additionally depends on the bandwidth of the pressure sensor, analog signal conditioning, anti-aliasing filtering and time synchronization.
A high sampling rate alone does not guarantee correct peak value measurement.
| Parameter | Assumption or Calculation | Result |
|---|---|---|
| Normal operating pressure | Freely selected initial condition | 110 bar |
| Full-scale value | Pressure gauge 0 to 250 bar | 250 bar |
| Static accuracy class | Class 1.0 | ±2.5 bar under the relevant static test conditions |
| Actual pressure pulse | Freely selected example value | 190 bar |
| Pressure step magnitude | 190 bar – 110 bar | 80 bar |
| Pulse duration | Freely selected example value | 40 ms |
| Assumed time constant | Simplified first-order measuring system | 120 ms |
| Calculated indication after 40 ms | 110 + 80 · (1 – e-0.04/0.12) | 132.68 bar |
| Dynamic difference | 190 bar – 132.68 bar | 57.32 bar |
| Data acquisition rate | 1,000 samples per second | 1 ms sampling interval |
8.8 Practical Interpretation
The calculation example illustrates a fundamental difference:
A mechanical maximum pointer can indicate that the measuring mechanism has reached a particular maximum position since its last reset.
However, it does not prove that the process pressure never exceeded this value.
Likewise, the time constant of a mechanical pressure gauge cannot simply be calculated backward from the difference between a maximum pointer reading and an electronically measured peak.
Such a determination would require a defined dynamic test procedure and a suitable model of the complete measurement chain.
Important: The 120 ms used in this example is exclusively a model assumption. The actual dynamic characteristics of a specific maximum pointer pressure gauge must be determined separately or supported by manufacturer specifications.
9. Distinguishing Pressure Spikes, Pulsations and Pressure Surges
In practice, the term pressure spike is used for very different types of events.
To select a suitable pressure gauge, it is necessary to clarify how these events arise and how long they last.
9.1 Individual Pressure Spike
An individual pressure spike is a temporary pressure increase above the previous pressure level.
It may occur, for example, during a rapid valve switching operation.
Its duration can vary considerably depending on the application.
9.2 Recurring Pressure Pulsations
Pulsations are recurring pressure fluctuations.
They may be caused, for example, by positive displacement pumps, piston movements or cyclic valve operations.
Repeated loading can mechanically stress both the measuring element and the pointer mechanism.
9.3 Pressure Surge
A pressure surge can occur, for example, when a flowing liquid is decelerated very rapidly.
Pressure waves may propagate through hydraulic lines as a result.
The magnitude and duration depend, among other factors, on flow velocity, fluid compressibility, pipeline elasticity and switching characteristics.
It is therefore not permissible to directly equate steady-state system pressure with a short-term pressure surge.
9.4 Mechanical Vibration
A fluttering pressure gauge pointer can also be influenced by mechanical vibrations within the plant.
Pointer movement is therefore not always clear evidence of an equally large actual process pressure fluctuation.
9.5 Significance for the Maximum Pointer
The maximum pointer cannot independently distinguish between a genuine pressure surge, a pulsation or mechanical pointer oscillation.
It simply retains the highest mechanically reached position.
The cause must be determined by investigating the overall system and measurement behavior.
10. Pointer Inertia, Friction and Mechanical Hysteresis
The pointer mechanism of a pressure gauge contains mechanical transmission elements that move in response to pressure changes.
Its dynamic behavior is determined, among other factors, by their mass, stiffness, friction and damping.
10.1 Inertia
A moving mass cannot change its velocity instantaneously.
During rapid pressure changes, the mechanical measuring system requires time to reach a new position.
This can cause a delayed indication.
10.2 Friction in the Pointer Mechanism
Mechanical friction can prevent small or rapid pressure changes from being fully converted into pointer movement.
The maximum pointer adds the retaining torque required for maximum value storage.
If the driving mechanism is stiff, this additional mechanical load can adversely affect the indication behavior.
10.3 Hysteresis
In pressure measurement, hysteresis describes, among other things, the difference in indication at the same test pressure during increasing and decreasing pressurization.
It can be influenced by the elastic and mechanical properties of the measuring system.
A maximum pointer must not obscure these differences as independent information about the actual process pressure.
10.4 Resonance and Overshoot
The mechanical system can have its own natural frequencies.
If these frequencies are excited, unexpectedly large pointer deflections can occur.
A maximum pointer can retain such a deflection even if it does not correspond to the highest quasi-static pressure value.
10.5 Aging and Wear
Repeated loading, vibration and long periods of operation can change the behavior of the measuring mechanism.
A maximum pointer pressure gauge with unusual or stiff pointer movement should therefore not continue to be used for important diagnostic tasks without inspection.
11. Evaluating Case Filling, Restrictors and Pressure Snubbers
Mechanical pressure measuring instruments are often protected against pulsations and vibrations by additional measures.
A distinction must be made between damping inside the pressure gauge and damping of the pressure signal before it reaches the measuring element.
11.1 Liquid-Filled Pressure Gauges
In liquid-filled pressure gauges, a suitable filling fluid is contained within the case.
It reduces the effects of vibration on the measuring mechanism in particular and can improve readability.
Typical filling media include glycerin, suitable glycerin-water mixtures or silicone oils, depending on the configuration and operating temperature.
Case filling protects mechanical components but does not automatically turn the instrument into a fast-responding peak value measuring device.
11.2 Restrictor in the Process Connection
A restrictor limits rapid pressure transmission through the connection path.
This can reduce pulsating loads on the measuring element.
At the same time, short pressure spikes at the actual process location may differ significantly from the profile detected by the pressure gauge.
11.3 Pressure Snubbers
Suitable pressure surge dampers or snubbers can be used for strongly fluctuating process pressures.
They must be selected according to the process medium, viscosity, temperature, pressure range and susceptibility to contamination.
Excessive damping may cause the pressure gauge to indicate short-term pressure increases only to a very limited extent.
11.4 Conflict Between Protection and Peak Detection
In many applications, there is a conflict between two objectives:
Effective damping is intended to protect the mechanical pressure gauge against destructive pulsations.
Accurate detection of the original rapid pressure spikes, on the other hand, requires sufficiently dynamic pressure measurement.
If necessary, these two tasks should be performed using different measuring systems.
11.5 Parallel Measurement
One practical solution may be to use a robust, appropriately damped pressure gauge for local process indication while installing a sufficiently fast pressure sensor in parallel for time-resolved diagnostics.
The measuring points, connection conditions and dynamic characteristics must be properly designed for both systems.
12. Influence of Measuring Lines and Connection Volumes
Not only the pressure gauge itself but also its mechanical connection to the process can influence the pressure signal.
12.1 Long Pressure Measuring Lines
A longer measuring line has a certain internal volume and mechanical properties.
In combination with the medium and the connected measuring instrument, time-dependent transmission effects may occur.
The pressure signal arriving at the gauge may therefore be delayed or altered compared with the pressure directly at the process location.
12.2 Trapped Gas Volumes
In hydraulic systems, trapped gas bubbles can strongly influence dynamic behavior.
Because gases are much more compressible than liquids, an additional gas volume can change the response of the measurement path.
It must therefore not be assumed without verification that a mechanically correctly connected measuring line also provides dynamically undistorted measurements.
12.3 Restrictions and Contamination
Very narrow connection bores or contaminated restrictors can slow pressure transmission.
This can result in a sluggish measuring pointer and correspondingly lower retained maximum pointer readings during short events.
12.4 Resonances
Line geometry, the medium and connection volume can amplify or attenuate certain dynamic frequencies.
Depending on the application, this can produce unexpected pressure oscillations at the measuring point.
12.5 Comparing Measuring Points
If two measuring instruments are installed at different process locations, a deviation may be caused by genuine local pressure differences.
The positions and connection paths must therefore be documented when comparing measurements.
13. Process Media, Materials and Temperature Limits
The pressure gauge must be selected according to the actual process medium.
The materials of the measuring element and process connection that come into contact with gases or liquids are particularly important.
13.1 Hydraulic Oils
For hydraulic applications, factors such as seal compatibility, operating temperature, contamination and possible pressure spikes must be considered.
Liquid-filled pressure gauges may offer advantages in applications involving high vibration levels and dynamic loading.
13.2 Pneumatic Systems
For gaseous media, the permissible operating conditions of the respective pressure gauge and the required safety configuration must be observed.
Risk-based selection is particularly important at higher gas pressures.
13.3 Aggressive Process Media
Suitable stainless steel pressure gauges or special material configurations may be used for aggressive media.
However, the general designation stainless steel does not replace a specific material compatibility assessment.
13.4 Highly Viscous or Crystallizing Media
Highly viscous or crystallizing process media can block the measuring connection.
Special process connections or suitable diaphragm seals may be required for such applications.
The maximum pointer itself does not eliminate errors caused by an unsuitable process connection.
13.5 Medium Temperature
The permissible medium temperature may differ from the permissible ambient temperature of the pressure gauge.
At elevated temperatures, suitable protective or separating elements must be considered.
13.6 Filling Fluid and Ambient Temperature
The viscosity of a case filling depends on temperature.
As a result, damping behavior can change under different ambient temperature conditions.
For applications involving large temperature differences, the specific filling fluid must therefore be suitable for the environment and measurement task.
14. Correctly Resetting and Documenting the Maximum Pointer
The indication of a maximum pointer generally refers to the period since its last reset.
Without a clearly defined observation period, its diagnostic value is limited.
14.1 Resetting According to Manufacturer Instructions
For corresponding configurations, WIKA describes an adjustment lock in the window that allows the maximum pointer to be reset using the designated adjustment key.
The reset procedure must follow the instructions for the specific device configuration.
Forcibly turning the adjustment lock or interfering with the window is not permitted.
14.2 Protecting the Window
Improper operation can damage the window.
For filled instruments, a damaged window can also cause the case filling fluid to escape.
The operating procedure specified by the manufacturer must therefore be followed.
14.3 Defining the Observation Period
Before a planned observation, the time at which the maximum pointer was reset should be documented.
This may be done, for example, before the start of an approved machine cycle or at the beginning of a maintenance interval.
14.4 Documenting the Reading
For a traceable record, at least the following information should be recorded:
- Designation of the measuring point.
- Pressure gauge model, measuring range and, where applicable, serial number.
- Date and time of the last reset.
- Current pressure value at the time of reading.
- Position of the maximum pointer.
- Known operating events during the observation period.
- Abnormalities or visible damage.
14.5 After an Event
If an unexpectedly high maximum pointer position is observed, its position should first be documented.
Resetting must not result in the loss of important information needed for a technical investigation.
Whether restarting operation is permissible depends on the company’s safety procedures and the assessment of the event detected.
15. Dynamic Measurement and Electronic Peak Value Detection
Time-resolved electronic measurement may be necessary for accurately evaluating short pressure spikes.
This applies particularly when not only the highest indicated value but also the duration, shape and recurrence of pressure events are relevant.
15.1 Pressure Sensor and Bandwidth
A pressure sensor suitable for dynamic measurements must be capable of detecting the relevant frequency components of the pressure profile.
Static accuracy alone does not describe this characteristic.
Bandwidth, response behavior, overpressure capability and output signal characteristics are particularly important.
15.2 Sampling Rate
Data acquisition must be sufficiently fast to resolve relevant pressure events over time.
An excessively low sampling rate may cause a short pressure pulse to occur between two measurement points and therefore not be fully captured.
15.3 Anti-Aliasing
Suitable data acquisition requires appropriate analog bandwidth limiting before digitization.
Otherwise, higher-frequency signal components may appear as apparent lower-frequency measured value fluctuations.
15.4 Digital Maximum Value Memory
An electronic peak value function can store the highest digitally captured value since the last reset.
However, measurement rate, filtering, measuring range and, where applicable, internal update times must be known to assess its significance.
15.5 Time-Dependent Pressure Curve
A complete pressure-versus-time recording can provide additional information about the course of a pressure spike.
For example, it can distinguish whether a pressure value occurred only very briefly or persisted over a longer period.
A purely mechanical maximum pointer does not provide this information.
15.6 Electronic Measurement Is Not Automatically Safety-Related
Even an electronic pressure sensor with fast data acquisition is not suitable for a safety-related monitoring function solely because of its measurement speed.
A safety-related function requires corresponding design and evaluation of the complete function.
16. Calibration, Functional Testing and Repeatability
Calibration verifies the relationship between a known reference pressure and the indication of the pressure gauge.
For a maximum pointer pressure gauge, it is additionally necessary to check whether the maximum value pointer performs its intended function correctly.
16.1 Static Pressure Calibration
During static calibration, the pressure gauge is compared with a suitable pressure standard.
The reference must be appropriate for the measuring range, measurement uncertainty and pressure type required by the test.
The test is performed at defined pressure points under suitable and stable conditions.
16.2 Increasing and Decreasing Pressure Points
Testing during increasing and decreasing pressurization allows deviations and hysteresis, among other characteristics, to be evaluated.
During such a test, the maximum pointer must be handled in a way that prevents its mechanical driving action from unintentionally influencing the intended measurement.
16.3 Functional Testing of the Maximum Pointer
The additional maximum pointer function can be examined using a suitable test procedure specified by the manufacturer.
The following points should be checked, among others:
- Whether the main pointer carries the maximum pointer along during a suitable pressure increase.
- Whether the maximum pointer remains in position after pressure reduction.
- Whether the maximum pointer can be reset correctly.
- Whether mechanical abnormalities such as sticking or unusual friction are apparent.
16.4 Calibration of the Maximum Pointer
A calibration certificate for the static pressure gauge indication does not automatically provide proof of accurate peak value detection by the additional maximum pointer.
If a quantitative statement about the maximum value indication is required, the actual scope of testing must be defined accordingly.
16.5 Dynamic Testing
Dynamic testing examines the behavior of the measuring system under defined time-dependent pressure profiles.
It requires a suitable test system and a sufficiently fast reference measurement path.
Ordinary static calibration does not replace this investigation.
16.6 Test Intervals
Suitable calibration and inspection intervals depend on the application, frequency of loading, ambient conditions and quality requirements.
After exceptional overpressure loading or unusual pointer behavior, an unscheduled inspection may be necessary.
17. Measurement Uncertainty and the Significance of the Retained Maximum
The uncertainty of a maximum pointer reading cannot be determined solely from the accuracy class of the pressure gauge.
Several different influencing factors must be taken into account.
17.1 Static Accuracy Class
The static accuracy class describes the error limits of the normal indication under the specified test conditions.
This information can provide a basis for evaluating a slowly reached pressure value.
17.2 Additional Mechanical Driving Mechanism
The maximum pointer has its own mechanical function.
Friction, retaining torque and possible reading differences can contribute additional deviations.
17.3 Dynamic Deviation
Short pressure events can occur more rapidly than the movement of the measuring mechanism.
The resulting deviation depends on the application and must be determined separately if necessary.
17.4 Influence of Installation
Restrictors, measuring lines and connected volumes can influence the pressure change arriving at the measuring mechanism.
The actual pressure spike at the process location may therefore differ from the time-dependent pressure at the measuring element.
17.5 Reading Uncertainty
Scale division, pointer width, parallax and lighting influence the reading.
The red maximum pointer also has a finite width, so its position cannot be determined with unlimited precision.
17.6 No Universal Correction Factor
It is not permissible to correct an assumed dynamic deviation simply by adding a fixed amount to the maximum pointer reading.
Such a correction would only be justified if supported by a suitable investigation and an applicable dynamic model.
Without this information, the mechanically retained value remains a diagnostic indicator rather than a fully validated process peak pressure value.
18. Operational Safety, Protective Functions and Limit Values
A maximum pointer pressure gauge can make pressure abnormalities easier to detect.
However, it does not prevent dangerous overpressure conditions.
18.1 Distinguishing Indication from Protective Functions
The maximum pointer is an additional mechanical indication function.
It does not replace pressure limitation, suitable switching functions or safety-related shutdown systems.
18.2 Safety Version of the Pressure Gauge
Certain applications involve increased requirements for case safety.
For Bourdon tube pressure gauges, EN 837-1 describes safety versions with corresponding protective measures, among other requirements.
For a safety version S3, the protection concept includes a solid baffle wall between the measuring system and dial, together with a blow-out back.
18.3 Gaseous Media
With gaseous media, failure of the pressure measuring system can present particular hazards.
The specific safety version must be selected according to operating conditions and the relevant manufacturer or standard requirements.
18.4 Overpressure Limits
The maximum pointer does not increase the overpressure resistance of the Bourdon tube measuring element or the pressure resistance of the process connection.
A retained maximum value close to full scale should prompt an examination of operating conditions and permissible pressure loading.
18.5 Pressure Spikes as a Possible Cause of Damage
Repeated pressure surges can stress not only the pressure gauge but also other components of a system.
An unusual maximum pointer position may therefore indicate the need for a more detailed process investigation.
18.6 Limitations of Mechanical Monitoring
A purely mechanical maximum pointer cannot automatically evaluate the duration or frequency of events.
If the safety of a system depends on certain pressure limits not being exceeded, an appropriately designed protective system is required.
19. Typical Applications in Mechanical and Plant Engineering
Maximum pointer pressure gauges can be useful in numerous industrial applications where monitoring temporary pressure increases is the main objective.
19.1 Hydraulic Power Units
In hydraulic systems, switching operations, load changes and pressure-limiting functions can cause short-term pressure changes.
A maximum pointer can indicate whether elevated mechanical pressure indications have occurred since its last reset.
19.2 Pumps
Different operating conditions can cause pressure fluctuations in pumps.
A mechanical maximum value indication can support operational monitoring.
However, appropriate damping is essential when strong pulsations occur.
19.3 Compressors
Compressor systems can also exhibit recurring pressure fluctuations.
The pressure gauge must therefore be selected with consideration for dynamic loading and the gas used.
19.4 Test Benches
On test benches, a maximum pointer pressure gauge can be used as an additional visual check.
However, a separate dynamic measurement may be necessary for quantitative verification of defined rapid pressure peaks.
19.5 Pressure Accumulators
In hydraulic accumulator systems, monitoring the maximum operating pressure can contribute to troubleshooting.
The hydraulic system pressure, any gas precharge pressure and the actual measuring points must be clearly distinguished.
19.6 Maintenance and Preventive Servicing
A maximum pointer can help identify unusual operating conditions between inspections.
Its diagnostic value increases when reset times and observed maximum values are documented systematically.
20. Systematic Testing and Commissioning Procedure
A systematic procedure is recommended for installing and using a maximum pointer pressure gauge.
- Define the measurement task: Determine whether a mechanically retained maximum value is sufficient or whether time-resolved pressure peak measurement is required.
- Record process conditions: Document normal pressure, maximum possible pressure loading, medium, temperature and dynamic behavior.
- Select the measuring range: Determine full scale and permissible continuous pressure loading according to the device specification.
- Check the safety version: Consider required case safety and personnel protection measures.
- Select materials: Check the compatibility of wetted components and seals.
- Define the process connection: Check the thread, sealing principle, connection location and installation conditions.
- Confirm the maximum pointer option: Verify that the actual ordered device configuration includes the required mechanical maximum value function.
- Evaluate damping: Determine whether case filling, a restrictor or a snubber is necessary and how these affect the intended measuring function.
- Install the measuring point: Carry out installation according to manufacturer specifications and the approved system procedure.
- Check leak tightness: Inspect the measuring point using the specified test procedure.
- Check the zero point: Verify the indication under a suitable reference condition.
- Perform a static functional test: Compare the pressure indication with a suitable reference.
- Check the maximum pointer function: Verify mechanical driving, retention and resetting according to the manufacturer’s specifications.
- Document the reset: Record a clearly defined beginning of the observation period.
- Monitor operation: Observe the movement of the main and maximum pointers during approved operation.
- Read the maximum value: Document the maximum pointer position and current pressure value separately.
- Evaluate abnormalities: Do not interpret unexpectedly high values as exact actual maximum pressures without further examination.
- Provide reference measurement if necessary: Use an electronic measuring system with suitable dynamic characteristics for short pressure events.
- Check the instrument condition: After unusual pressure events, assess whether the pressure gauge requires inspection or replacement.
- Document the results: Record measurement conditions, device data, results and actions taken in a traceable manner.
Resetting the maximum pointer and any intervention at the measuring point may only be carried out according to the manufacturer’s instructions and the operationally approved procedure.
21. Typical Fault Symptoms and Targeted Diagnostics
When unusual maximum pointer positions occur, a distinction must first be made between mechanical malfunctions and actual process pressure changes.
The following fault symptoms illustrate typical causes and suitable diagnostic approaches.
| Fault Symptom | Possible Cause | Suitable Diagnostic Action |
|---|---|---|
| Maximum pointer remains considerably below an electronically measured pressure peak | Short pressure pulse, mechanical inertia, damping or different measuring points | Compare measuring points and time profiles; check the dynamic characteristics of the complete measurement chain |
| Maximum pointer indicates an unusually high value | Actual pressure increase or mechanical overshoot | Investigate operating events and, if necessary, perform time-resolved reference measurement |
| Maximum pointer is not carried along | Stiff movement, incorrect position or damaged driving mechanism | Perform a functional test according to manufacturer specifications |
| Maximum pointer moves backward together with the main pointer | Insufficient retaining force or mechanical damage | Check retaining function and instrument condition |
| Reset mechanism is difficult to operate | Mechanical malfunction, contamination or improper operation | Check the adjustment mechanism according to the manufacturer’s instructions; do not apply force |
| Main pointer fluctuates strongly | Pressure pulsations, vibrations or mechanical resonance | Distinguish process pressure from ambient vibrations and evaluate damping |
| Pressure gauge responds slowly | Restriction, narrowed process connection, long measuring line or strong damping | Check the connection path and dynamic pressure transmission |
| Pressure gauge indicates a zero-point error after an event | Possible overpressure, permanent deformation or mechanical damage | Perform an unscheduled inspection and replace the instrument if necessary |
| Two mechanical pressure gauges give different indications | Different accuracy, installation conditions, damping or local pressure differences | Perform a static comparison test and evaluate the measuring points |
| Maximum pointer position cannot be assigned to an event | Time of last reset is unknown | Introduce a documented observation period |
| Window or case filling is damaged | Mechanical damage or incorrect resetting procedure | Take the instrument out of service according to a safe procedure and inspect it |
The listed causes are possible diagnostic explanations and do not constitute definitive fault identification.
Particularly for safety-related pressure events, evaluation must be based on suitable measurements and the specified system procedure.
22. Suitable ICS Products and Selection Options
ICS Schneider Messtechnik offers various mechanical pressure measuring instruments for mechanical engineering, hydraulics, pneumatics and the process industry.
For a maximum pointer, it is essential that the required additional function is available for the specific pressure gauge configuration and compatible with its other equipment features.
22.1 WIKA PG23CP – Bourdon Tube Pressure Gauge for Panel Mounting
The WIKA PG23CP is an industrial Bourdon tube pressure gauge made of stainless steel for installation in operating and control panels.
It is suitable, for example, for industrial hydraulic power units, wellhead control panels and process industry applications.
Documented features include:
- Bourdon tube measuring principle according to EN 837-1 or ASME B40.100.
- Nominal sizes 63 and 100 mm.
- Indication ranges up to 1,600 bar, depending on configuration.
- Accuracy class 1.6 for NS 63 or class 1.0 for NS 100 according to EN 837-1.
- Fully welded mounting ring for suitable panel installations with IP66 protection.
- Versions with safety levels S1 and S3.
- Optional case fillings depending on configuration.
- Configurable red maximum pointer on the window according to WIKA data sheet PM 02.24, edition 12/2024.
The PG23CP is therefore particularly interesting when a compact, easily readable local pressure indication with a documented maximum pointer option is required.
However, the red maximum pointer is an optional feature and is not automatically included in every available PG23CP configuration.
When ordering, the measuring range, nominal size, safety level, case filling, connection variant and maximum pointer must therefore be explicitly specified.
The same limitation applies to this instrument: the maximum pointer option alone does not guarantee complete detection of arbitrarily short pressure spikes.
Further Information: WIKA PG23CP at ICS Schneider Messtechnik
22.2 WIKA 232.50 and 233.50 – Stainless Steel Bourdon Tube Pressure Gauges
The WIKA models 232.50 and 233.50 are stainless steel Bourdon tube pressure gauges for industrial and process applications.
They are available, among other applications, for gaseous and liquid media that are neither highly viscous nor crystallizing.
Important documented features include:
- Mechanical Bourdon tube measuring system.
- Wetted components made of stainless steel.
- Nominal sizes 63, 100 and 160 mm.
- Indication ranges up to 1,600 bar, depending on nominal size.
- Accuracy class 1.6 for NS 63 and class 1.0 for NS 100 or NS 160.
- Model 233.50 with case filling for suitable applications involving dynamic loading.
- Various process connections and configuration options.
These instruments are particularly interesting when the media compatibility of a stainless steel measuring system and robust local indication are the main priorities.
For the required maximum pointer function, availability and compatibility with the other options must be confirmed for the specific ordered configuration within this model series.
A maximum pointer is not assumed to be a standard feature across the series.
Further Information: WIKA 232.50 / 233.50 at ICS Schneider Messtechnik
22.3 WIKA 232.30 and 233.30 – Safety Bourdon Tube Pressure Gauges
The WIKA models 232.30 and 233.30 are designed for applications with increased personnel protection requirements.
The pressure gauges feature an S3 safety configuration with a solid baffle wall between the measuring system and dial, as well as a blow-out back.
Documented features include:
- Design according to EN 837-1 and ASME B40.100.
- Wetted components made of stainless steel.
- For suitable gaseous and liquid process media.
- Indication ranges from 0 to 0.6 bar up to 0 to 1,600 bar in the specified configurations.
- High resistance to pressure cycling and mechanical shocks.
- Model 233.30 with case filling for demanding dynamic operating conditions.
This product family is particularly suitable for consideration when the appropriate safety version is a decisive selection criterion.
Whether a maximum pointer is available in the desired combination of nominal size, safety version and case filling must be verified for the specific configuration.
The maximum pointer must not impair the safety-related characteristics of the pressure gauge.
Further Information: WIKA 232.30 / 233.30 at ICS Schneider Messtechnik
22.4 WIKA 213.53 – Liquid-Filled Industrial Bourdon Tube Pressure Gauge
The WIKA 213.53 is a liquid-filled mechanical Bourdon tube pressure gauge for industrial applications involving increased dynamic loading and vibrations.
The instrument has a stainless steel case and wetted components made of copper alloy.
Documented features include:
- Mechanical Bourdon tube measuring system according to EN 837-1 or ASME B40.100.
- Nominal sizes 50, 63 and 100 mm.
- Indication ranges up to 1,000 bar, depending on configuration.
- Case filling to damp vibrations and dynamic loading.
- IP65 protection.
- Accuracy class up to class 1.0 in suitable configurations.
- Various connection positions and panel mounting options.
The WIKA 213.53 is a potential solution for robust local pressure indications in hydraulic, pump and compressor applications, provided the media used do not attack the wetted copper alloys.
However, it is not automatically equipped with a maximum pointer. If this function is required, actual availability for the specific configuration must be requested.
Due to the case filling, it must also be checked whether the intended monitoring of short pressure events is compatible with the dynamic characteristics of the instrument.
Further Information: WIKA 213.53 at ICS Schneider Messtechnik
22.5 Supplementing Mechanical Indication with Electronic Pressure Measurement
If accurate detection of short pressure spikes is required, additional electronic pressure measurement may be useful.
In this arrangement, the mechanical pressure gauge is used for local monitoring, while a suitable pressure sensor records the time-dependent pressure profile.
When selecting such a measurement chain, the following characteristics are particularly important:
- Appropriate pressure measuring range.
- Sufficient dynamic bandwidth.
- Suitable process connection.
- Media and temperature compatibility.
- Suitable output signal.
- Sufficient data acquisition sampling rate.
- Appropriate analog filtering.
- Traceable time-based documentation.
Electronic measurement does not automatically replace a required safety function and must be designed for its suitability in the respective application.
Pressure Measurement Technology at ICS Schneider Messtechnik
22.6 Selection Criteria for a Quotation Request
For a suitable pressure gauge configuration with a maximum pointer, the following information should be provided in particular:
- Normal operating pressure.
- Maximum expected process pressure.
- Required indication range.
- Process medium, including temperature and any aggressive components.
- Frequency and approximate duration of pressure pulsations or pressure spikes.
- Required accuracy class.
- Nominal size and reading distance.
- Process connection and connection position.
- Mounting method, such as direct mounting or panel mounting.
- Existing vibrations and possible need for case filling.
- Required safety version.
- Explicitly required maximum pointer with a suitable reset mechanism.
- Any additional calibration or dynamic reference measurement required.
Based on this information, it is possible to assess which pressure gauge family is suitable and whether mechanical maximum value indication is sufficient for the intended measurement task.
23. Conclusion: Using the Maximum Pointer Correctly as a Diagnostic Indicator
A pressure gauge with a maximum pointer offers a simple and practical way to make temporary pressure increases visible even after the actual event has ended.
Particularly in mechanical and plant engineering, mechanical maximum value indication can provide valuable information about unusual operating conditions that would remain unnoticed during an occasional check of the normal measuring pointer.
However, the function has one essential limitation: the maximum pointer retains the highest position reached by the mechanical measuring mechanism. It does not store a complete time-dependent process pressure profile and does not automatically measure the actual highest pressure of a very short event.
During dynamic pressure events, the inertia of the measuring element, friction in the pointer mechanism, the driving mechanism and the damping used can result in pressure spikes being displayed only partially.
Under other dynamic conditions, mechanical oscillations can also cause excessive pointer deflection.
A retained maximum pointer value is therefore neither necessarily an exact upper limit nor a reliably determined absolute maximum process pressure.
Several points are therefore essential for correct application.
First, the mechanical maximum pointer function must actually be available for the selected device configuration. A red reference pointer and a red maximum pointer perform different tasks.
Second, the measuring range, continuous pressure loading capability, overpressure resistance, media compatibility and safety version must be selected correctly.
Third, installation conditions influence the measurement. Long connecting lines, restrictors and other damping components can change the pressure profile at the gauge compared with the actual process.
Fourth, the time of the maximum pointer reset should be documented. Without a defined observation period, an indicated maximum can only be assigned to an operating event to a limited extent.
Fifth, additional dynamic pressure measurement is often required for quantitative detection of short pressure spikes.
A maximum pointer pressure gauge and an electronic pressure sensor can therefore complement each other effectively: the mechanical instrument provides straightforward local maximum value indication, while a suitable electronic system examines the actual time-dependent pressure profile.
The key conclusion is: A maximum pointer indicates the highest value reached by the mechanical measuring mechanism. Whether this value corresponds to the actual highest process pressure depends on the dynamic behavior of the complete measuring arrangement.
24. Frequently Asked Questions About Pressure Gauges with Maximum Pointers
24.1 What Is a Pressure Gauge with a Maximum Pointer?
A pressure gauge with a maximum pointer has an additional mechanical pointer for maximum value indication alongside the normal measuring pointer. As the indicated pressure increases, the maximum pointer is carried along by the main pointer. When the indication subsequently decreases, the maximum pointer remains at the highest position reached. This makes a previously indicated higher pressure visible even after the event.
24.2 How Does a Mechanical Maximum Pointer Work?
In corresponding WIKA configurations, the pointer is driven by a mechanical driving pin. The normal measuring pointer moves the maximum pointer toward higher scale values as the indication rises. When the indication decreases, the maximum pointer is not moved backward. The retained position can subsequently be reset using the designated reset mechanism.
24.3 Does a Maximum Pointer Indicate the Actual Maximum Pressure?
Not necessarily. It indicates the highest mechanically reached value. During very short pressure spikes, inertia, friction and damping can prevent the pointer mechanism from reaching the actual process pressure. Conversely, mechanical oscillations can cause excessive pointer deflection. For precise dynamic peak value measurement, the complete measurement chain must be appropriately designed and tested.
24.4 Why Does My Maximum Pointer Show a Lower Value Than an Electronic Pressure Sensor?
One possible reason is the difference in dynamic response. A fast electronic pressure sensor can detect a short pressure spike, while a mechanical pressure gauge may indicate only a lower maximum due to its inertia and damping. Differences in measuring location, measuring range and signal processing must also be considered. The instruments should be tested under comparable conditions.
24.5 Can a Maximum Pointer Also Indicate a Value That Is Too High?
Yes, this is possible under certain conditions. Mechanical oscillations, resonances or overshoot of the pointer mechanism can cause a deflection that does not correspond to the actual quasi-static pressure value. The maximum pointer can retain this deflection. An unusually high indication should therefore initially be treated as evidence of an event requiring investigation rather than automatically as exact proof of pressure.
24.6 What Is the Difference Between a Maximum Pointer and a Reference Pointer?
A maximum pointer is mechanically driven by the measuring pointer and retains a maximum indicated position. A reference pointer, by contrast, is used to visually mark a particular value on the scale. For example, it can indicate a setpoint or an operating limit. A reference pointer normally does not store an actual maximum value reached.
24.7 How Do You Reset a Maximum Pointer?
On corresponding WIKA pressure gauges, resetting is performed using an adjustment lock in the window and a designated adjustment key. The specific procedure is described in the instrument’s operating instructions. Forcible operation must be avoided because it can damage the window. On filled pressure gauges, damage may also cause the case filling fluid to escape.
24.8 Does the Maximum Pointer Need to Be Reset After Every Measurement?
This depends on the intended observation period. If the maximum indicated value is to be recorded during a particular operating cycle, the beginning of that observation must be clearly defined. If the highest value is to be retained over a maintenance interval, the maximum pointer may remain in position for a correspondingly longer period. The decisive factor is that resetting and reading are documented in a traceable manner.
24.9 Can a Maximum Pointer Pressure Gauge Measure Pressure Spikes in the Millisecond Range?
Whether a pressure event in the millisecond range can be adequately detected depends on the dynamic characteristics of the specific pressure gauge and its installation. A conventional mechanical maximum pointer provides no general guarantee of precise detection of such short events. If this measurement capability is required, a sufficiently fast pressure sensor with suitable data acquisition is necessary.
24.10 Is a Glycerin-Filled Pressure Gauge with a Maximum Pointer Better?
Glycerin filling can reduce the effects of vibration and protect the mechanical measuring mechanism. This may be advantageous for strongly vibrating machinery. At the same time, it must be checked how the damping influences the desired maximum value indication. Case filling does not automatically mean that the pressure gauge captures short pressure spikes more completely.
24.11 What Accuracy Does a Pressure Gauge with a Maximum Pointer Have?
Static accuracy depends on the selected pressure gauge configuration and its accuracy class. For example, class 1.0 with an indication range of 0 to 250 bar corresponds to a static error limit of ±2.5 bar under the relevant test conditions. However, an equally small error limit for detecting arbitrarily short pressure spikes cannot be derived from this specification.
24.12 Which Measuring Range Should a Maximum Pointer Pressure Gauge Have?
The measuring range must cover normal operating pressure and expected pressure increases. At the same time, permissible continuous pressure loading, overpressure resistance and required reading accuracy must be considered. The smallest possible measuring range is not always the best choice because pressure spikes may cause overloading. Correct sizing is based on the specific process conditions and manufacturer data.
24.13 Can a Maximum Pointer Replace a Pressure Switch?
No. A mechanical maximum pointer retains an indicated position and does not automatically provide an electrical switching function. If a signal must be triggered or a machine shut down at a certain pressure, suitable switching or safety equipment must be provided. A maximum pointer alone does not perform this function.
24.14 Why Does My Maximum Pointer Not Remain in Position?
If the maximum pointer moves backward together with the normal measuring pointer, the mechanical retaining function may be faulty. Damage or incorrect settings are also possible causes. Functional testing must follow the manufacturer’s specifications. Unauthorized intervention in the mechanical pointer mechanism should be avoided.
24.15 Why Is the Maximum Pointer Not Being Carried Along?
Possible causes include an unfavorable initial position, stiff movement or a damaged driving mechanism. The function should be examined using a suitable test procedure. Failure to carry the maximum pointer along must not automatically be taken as proof that no pressure increase occurred.
24.16 Is a Pressure Gauge with a Maximum Pointer Suitable for Hydraulic Applications?
Yes, maximum pointer pressure gauges can be used for suitable hydraulic measurement tasks. The measuring range, pressure pulsations, vibrations, medium temperature and necessary protective measures must be considered. Particularly with fast-switching valves or strongly pulsating pumps, it must be checked whether the mechanical indication is sufficient for the intended purpose or whether additional dynamic measurement is required.
24.17 Can a Maximum Pointer Pressure Gauge Be Calibrated?
The normal pressure indication can be calibrated statically using suitable pressure references. In addition, the mechanical driving and retaining function of the maximum pointer can be checked using an appropriate test procedure. However, static calibration does not automatically demonstrate accuracy during rapid pressure spikes. If the dynamic maximum value function must be evaluated quantitatively, a suitable separate scope of testing must be defined.
24.18 When Is an Electronic Pressure Sensor More Suitable Than a Maximum Pointer Pressure Gauge?
Electronic pressure measurement is particularly useful when very short pressure spikes, their duration, time-dependent profile or frequency of occurrence need to be investigated more precisely. This requires the sensor, connection path, signal processing and data acquisition system to be suitable for the required dynamic response. A mechanical maximum pointer pressure gauge can still provide a practical addition for local visual monitoring.